HOT-PLATE PLASTIC WELDING MACHINE
Description
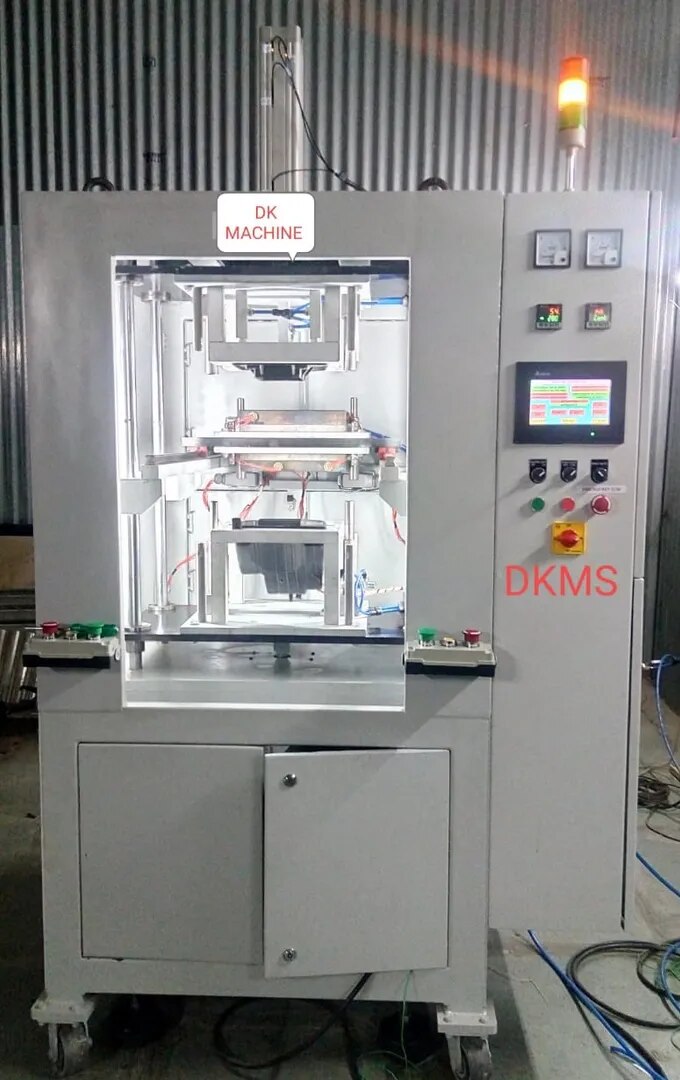
HOT-PLATE PLASTIC WELDING MACHINE
MODEL :- DK400H
POWER SUPPLY :- 415V 3 phase, Earth, A.C./50Hz with 1% tolerance, Stabilized /30A.
Power consumption :- estimated 20A peak
AIR PRUSSURE - 7 Kg /sq.cm , constant ,dry & free from dust particles 6-8 Kg
Important factors –
1. The welding results and consistency largely depends on quality of parts to weld like Warpage control, Dimensions and injection molding quality.
2. Melting temperature for heater plate expected 270-300ºC ± 10%. Please let us have your material data on this.
3. Machine Operation Sequence
• Operator Puts Machine ON to achieve Temperature set –Make ON Vacuum.
• Operator put an assembled plastic part into upper and lower fixture.
• Activate lower part support bracket holding.
• Operator press start button–—parts held in fixtures/jig.
• Auto cycle starts if temperature achieved – Both Fixture/jigs close together to match and get apart (this can by pass) in auto cycle ---Heater Plate comes forward—Upper jig (descent)and lower jigs (ascent) with parts moves toward hot plate – Gets pressed against heater plate – heating time – Material soften time --- Fixtures get apart to some distance --- Heater plate moves backward – Both Fixtures close together to join parts – Hold time (cooling time) – Time end – Vacuum for upper part released – Both jigs goes to Origin – Welded part remain in lower jig – Operator open bracket holding and un load part from lower fixture – cycle complete– New parts loaded by operator.
• Cycle program can be changed by suggestions, the one mentioned is better practice.
• Suggestions in features of machine will be considered . certain specification of
machine may change to suit to weld part of different height.
4. Cycle Time sequence estimate
• Machine Set ON - 25 min. to achieve temp. (first time )
• Operator put parts into fixture and press start button (8-10S)
• Heater plate comes forward and jigs close to it (3S)
• Melting + soak time Expected (depends on weld rib design) (8S)
• Jigs apart and Heater plate moves backward (3S)
• Holding time for cooling, Includes jig close in (20-30S)
• Both jigs retract back part remains in lower jig (2S)
• Operator unload part (3S)
• Cycle time depends on weld parameters, speed set, Weld line Dimensions so may vary and can set up on trials.
• Estimate Cycle time : 45-57S
• Based on above – Production per hour – 50 pcs.max.
• Based on above – Production for 8 hrs run – 400pcs max.
5. Important Overview
Safety Sensor Curtain Safety - Yes
Upper Part Vacuum /hold arrangement - Yes
Lower Part Vacuum/hold arrangement - Yes
Separate digital Temperature PID x 2 - Yes
Production counter (weld cycle) - Yes
Tool Interchangeability - Yes (manual -12-15 min.
except cooling and heating time)
PLC operation - Yes
Parameters Set on HMI - Yes
Compressed Air required - 0.7-0.8 Mpa/8bar constant, dust particle free.
Start by Two distant Push Switch - Yes
Emergency Push stop Switch - Yes
Pressure regulator and Display - Yes
Machine with Shoes and Castors - Yes
Two tube Lights in work area - Yes
4 Guide pillar Linear bearing support for precise Jig, Fixture tool movement –
- Yes.
Block Linear bearing drive for heater mold movement with end to end cushion to reduce impact, shock absorber cushion. - Yes
Part presence sensor (not required) - No
Pressure banker tank built in machine - Yes
